AEROSIL 200 Alternatives A Cost-Effective Replacement Option for Industrial Applications

For decades, AEROSIL® 200 has been one of the most recognized hydrophilic fumed silica grades in the global specialty chemicals market. Known for its excellent thickening efficiency, rheology control, and reinforcement performance, it has become a preferred choice across industries such as coatings, adhesives, sealants, silicone rubber, inks, and composites.

However, many manufacturers today are actively looking for cost-effective alternatives to AEROSIL 200 due to rising material costs, longer supply chains, and the need for more flexible sourcing options.

At Zhengzhou Gesee New Materials Co., Ltd., we developed GESEESIL A200 as a high-performance replacement solution designed to match the key characteristics of AEROSIL 200 while offering competitive commercial value.

Why Are Buyers Looking for Alternatives to AEROSIL 200?

While AEROSIL 200 has long set the benchmark for hydrophilic fumed silica, many downstream manufacturers are now facing practical challenges:

  • Increasing procurement costs
  • Supply fluctuations in some regional markets
  • Longer international lead times
  • Limited sourcing flexibility

For formulators, switching to an alternative is not only about price reduction. It is about finding a product that can deliver comparable rheological performance, stable quality, and reliable technical consistency.

That is where GESEESIL A200 offers a practical solution.

What Makes GESEESIL A200 Comparable?

GESEESIL A200 is a hydrophilic fumed silica with a specific surface area of approximately 200 m²/g, engineered to provide performance characteristics similar to AEROSIL 200 in demanding industrial formulations. Typical benchmark values for this class are around 180–220 m²/g BET surface area with high SiO₂ purity and strong dispersibility.

It provides:

  • Excellent thickening efficiency
  • Strong anti-settling performance
  • Effective thixotropic control
  • Good dispersibility in resin systems
  • Reliable reinforcement in silicone elastomers
  • Consistent batch-to-batch stability

These properties make it suitable for direct evaluation in existing formulations with minimal reformulation effort.

Typical Applications

GESEESIL A200 performs well in a wide range of industrial systems, including:

Coatings and Paints

Improves sag resistance, suspension stability, and flow control while enhancing storage stability.

Adhesives and Sealants

Provides viscosity adjustment and anti-slump properties for easier processing and improved application consistency.

Silicone Rubber

Acts as a reinforcing filler to improve tensile strength and mechanical performance.

Printing Inks

Helps control rheology and improves pigment suspension behavior.

Composite and Resin Systems

Enhances structural consistency while reducing filler sedimentation during storage.

Performance Meets Cost Efficiency

For many manufacturers, qualification of a new raw material depends on balancing technical performance with overall production economics.

GESEESIL A200 offers:

  • Competitive pricing compared with premium imported grades
  • Stable export supply
  • Flexible packaging solutions
  • Technical support for product evaluation
  • Faster response and customized cooperation options

This allows manufacturers to optimize production cost without sacrificing product quality.

How to Evaluate a Replacement Successfully

When replacing AEROSIL 200, we recommend evaluating:

  • Viscosity build-up behavior
  • Dispersion efficiency
  • Thixotropic recovery
  • Reinforcement effect
  • Final product appearance
  • Long-term storage stability

Our technical team can provide sample support and application guidance to help customers complete validation efficiently.

Looking for a Reliable AEROSIL 200 Alternative?

If your company is evaluating alternatives to imported fumed silica grades, GESEESIL A200 offers a practical balance of performance, consistency, and cost advantage.

At Zhengzhou Gesee New Materials Co., Ltd., we are committed to supplying high-quality fumed silica solutions for global industrial customers.

Contact us today to request technical data, samples, or application support.


Beat the Heat How Fumed Silica Insulation Helps Industries Stay Efficient During Summer

Summer Heat Brings New Challenges

As temperatures continue to rise during the summer months, industries around the world face increasing challenges in managing heat, reducing energy consumption, and maintaining stable production environments.

Whether it is chemical processing, metallurgy, battery manufacturing, or industrial furnaces, excessive heat not only increases operating costs but also reduces equipment efficiency and shortens service life. Choosing the right insulation material has become more important than ever.

Why High-Performance Thermal Insulation Matters

Traditional insulation materials often struggle under extreme temperatures. They may become bulky, lose insulation performance over time, or require greater thickness to achieve the desired thermal resistance.

Advanced thermal insulation materials help companies:

  • Reduce heat loss
  • Lower energy consumption
  • Improve workplace safety
  • Maintain process temperature stability
  • Reduce carbon emissions
  • Extend equipment service life

These benefits are particularly valuable during periods of high ambient temperatures.


The Role of Fumed Silica in Thermal Insulation

Fumed silica is an ultra-fine nanomaterial with an exceptionally high specific surface area and extremely low thermal conductivity.

Thanks to its unique three-dimensional particle network, fumed silica is widely used in:

  • High-performance insulation panels
  • Vacuum insulation panels (VIPs)
  • Industrial furnaces
  • High-temperature pipelines
  • New energy battery thermal management
  • Aerospace thermal insulation

Its outstanding thermal performance allows manufacturers to achieve excellent insulation while reducing material thickness and weight.


Fumed Silica Insulation Boards: Thin Yet Powerful

Fumed silica insulation boards combine nanoporous technology with premium fumed silica to deliver excellent thermal insulation performance.

Compared with conventional insulation materials, they offer several advantages:

  • Extremely low thermal conductivity
  • Lightweight construction
  • High compressive strength
  • Excellent fire resistance
  • Stable performance under high temperatures
  • Long service life
  • Space-saving thin design

These features make them suitable for industrial equipment, energy systems, buildings, cold-chain logistics, and other demanding applications.


Beyond Insulation: Fumed Silica for Multiple Industries

In addition to thermal insulation applications, fumed silica is widely used as a multifunctional additive across many industries.

Its excellent thickening, reinforcing, anti-settling, anti-sagging, and rheology-control properties make it an ideal choice for:

  • Silicone rubber
  • Sealants
  • Adhesives
  • Paints and coatings
  • Inks
  • Battery materials
  • Unsaturated polyester resin
  • Composite materials

As industries continue to seek higher performance and improved efficiency, demand for high-quality fumed silica continues to grow worldwide.


Why Choose GESEE?

At Zhengzhou GESEE New Materials Co., Ltd., we are committed to providing reliable, high-quality material solutions for customers around the world.

Our product portfolio includes:

  • Hydrophilic Fumed Silica
  • Hydrophobic Fumed Silica
  • Fumed Silica Thermal Insulation Boards

We support customers with stable quality, professional technical service, competitive pricing, and flexible global supply.

Whether you are looking for raw materials or advanced thermal insulation solutions, GESEE is ready to help your business improve efficiency and reduce energy consumption.


Conclusion

Summer heat is a reminder that effective thermal management is no longer optional—it is essential.

By selecting advanced fumed silica materials and high-performance insulation boards, companies can reduce energy costs, improve operational efficiency, and build more sustainable production systems.

If you are looking for reliable fumed silica products or thermal insulation solutions, feel free to contact Zhengzhou GESEE New Materials Co., Ltd. We are always ready to support your next project.

Fumed Silica The Core Power in Thermal Insulation Industry

Introduction

In today’s world where energy conservation and carbon emission control are increasingly valued, thermal insulation materials play a crucial role in both industrial and civil applications. Among a wide range of insulation materials, fumed silica—with its unique nanostructure, ultra-high specific surface area, and exceptional thermal insulation performance—is gradually becoming an indispensable core material in the thermal insulation industry. Moreover, vacuum insulation panels (VIPs) and high-performance insulation boxes made from fumed silica are demonstrating broad application prospects across multiple fields, including cold chain logistics, biopharmaceuticals, and fresh food preservation.


I. The Thermal Insulation Mechanism of Fumed Silica

Fumed silica is an amorphous nano-scale powder material produced through the high-temperature hydrolysis and condensation of silicon halides. Its primary particle size is only 7–40 nm, and its specific surface area can reach as high as 400 m²/g. Its excellent thermal insulation performance mainly stems from the following aspects:

First, the nano-porous structure. Fumed silica particles are connected by hydrogen bonds and van der Waals forces, forming a stable three-dimensional dendritic network structure. A large number of micro- and nano-scale air pores exist within and between the particles. Air itself is a poor conductor of heat, and these tiny pores effectively disrupt the continuity of heat conduction pathways, thereby significantly reducing the material‘s thermal conductivity

Second, the interfacial scattering effect. Numerous interfaces are formed between fumed silica nanoparticles and the base material. These interfaces scatter heat flow, effectively increasing thermal resistance and impeding heat transfer.

Third, infrared radiation blocking. The particle size of fumed silica is close to the wavelength of infrared thermal radiation, enabling strong scattering of infrared photons and blocking heat transfer through radiation. This infrared scattering effect is particularly significant in medium-to-high temperature environments.


II. Vacuum Insulation Panel (VIP): The Star Application of Fumed Silica
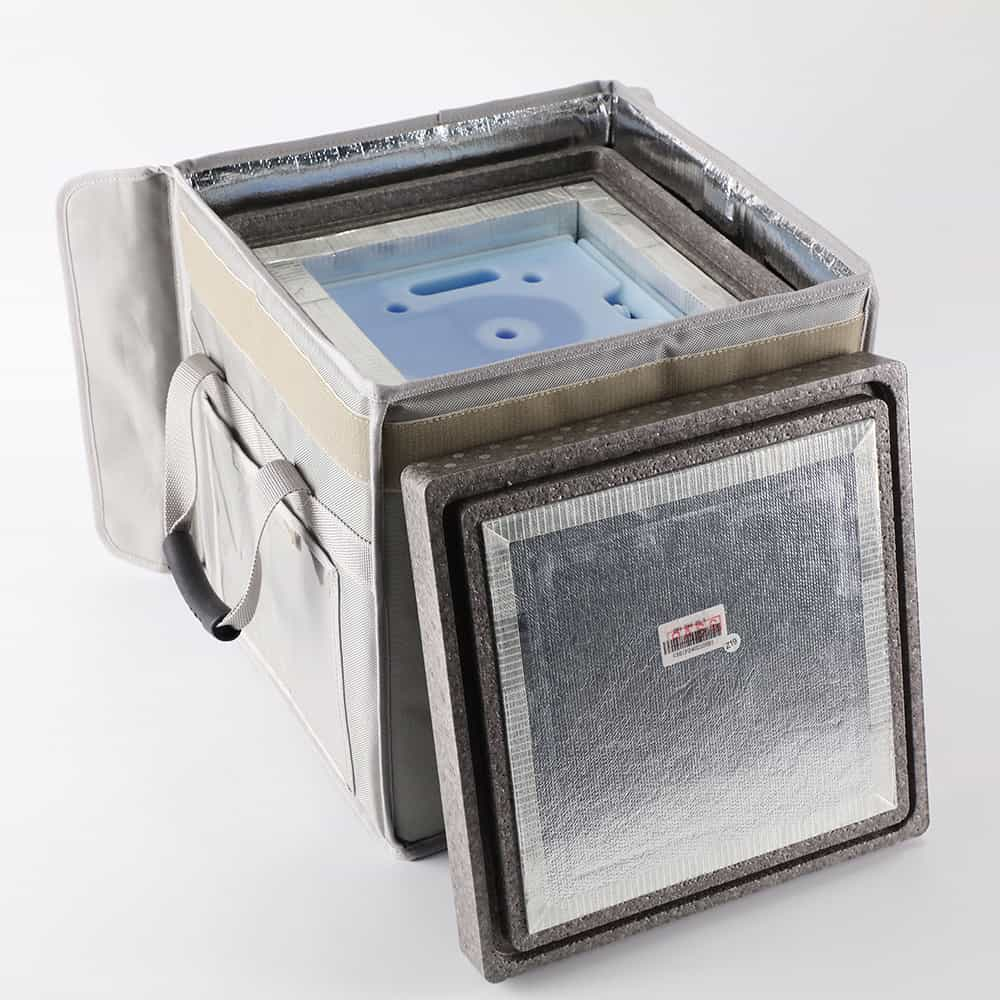
fumed silicaVIP BOARDVIP BOX

Vacuum insulation panel (VIP) is one of the most important application forms of fumed silica in the thermal insulation field. VIP primarily consists of three parts: the core material, the high-barrier envelope, and the getter. The choice of core material is the key factor determining VIP performance. Compared to traditional core materials such as glass wool and microsilica, fumed silica offers clear advantages in terms of manufacturing cost, production efficiency, thermal stability, and service life.

VIPs with fumed silica as the core material can achieve a thermal conductivity as low as 0.004–0.005 W/(m·K) (i.e., 4–5 mW/m·K), offering 5 to 10 times better thermal insulation performance compared to conventional insulation materials such as polyurethane foam. At the same time, VIPs are only 1/5 to 1/10 the thickness of traditional insulation materials, achieving a thinner, lighter product that provides a slimmer insulation layer, larger usable space, and lower overall weight for insulated chambers.

More notably, even if a VIP loses its vacuum under extreme circumstances, the fumed silica core material itself still provides good thermal insulation performance, outperforming most other insulation materials. This means that VIPs using fumed silica cores offer higher reliability and longer service life—some high-quality fumed silica core VIPs can last for 50 years or more.


III. Application Scenarios: From Cold Chain Logistics to Pharmaceutical Transport

Thanks to the exceptional thermal insulation performance of VIPs, fumed silica is widely used in various thermal insulation scenarios. In the field of cold chain logistics, insulation boxes using fumed silica VIPs as the core insulation material are gradually replacing traditional EPS (expandable polystyrene) foam boxes and are becoming the new benchmark in the industry.

Taking cold chain insulation boxes as an example, with VIPs (using nano-scale fumed silica as the core material) as the insulation material, less dry ice is needed to achieve longer temperature retention under the same conditions, effectively reducing energy consumption and costs. Meanwhile, the internal temperature inside the box is more stable and evenly distributed, ensuring product quality and safety during transport.

In the pharmaceutical cold chain field, the application of fumed silica VIPs is particularly significant. Temperature-sensitive biopharmaceuticals such as mRNA COVID-19 vaccines require storage and transport under extremely low temperatures of -70°C. VIP insulation boxes containing fumed silica use passive cooling methods without the need for external power, achieving precise temperature control and preventing temperature fluctuations, thus becoming a key link in ensuring the integrity of the vaccine supply chain.

The core advantages of fumed silica VIPs in low-temperature transport include:

  • Reliable passive cooling without external energy supply

  • Reduced energy consumption and CO₂ emissions

  • Slim-wall design increases transport and storage capacity by up to 20%

  • Lightweight for easy portability

  • Service life exceeding 30 years, offering sustainability

In addition, fumed silica VIPs are widely used in household refrigerators, yacht refrigerators, car refrigerators, deep freezers, electric water heaters, vending machines, building wall insulation, LNG storage and transport, and many other fields. It can be said that wherever efficient thermal insulation and energy saving are required, fumed silica is present.

IV. Market Trends and Prospects

The global fumed silica market is experiencing steady growth. According to market research data, the global fumed silica market is expected to grow from USD 1.80 billion in 2025 to USD 2.14 billion by 2030, at a compound annual growth rate (CAGR) of approximately 3.46%. Meanwhile, the fumed silica vacuum insulation panel (VIP) sub-market is performing particularly well: the global fumed silica VIP market was valued at approximately USD 296 million in 2024 and is projected to reach USD 536 million by 2031, with a robust CAGR of 9.2%.

The main drivers of this growth include:


  • Growing global emphasis on energy efficiency and sustainable development

  • Increasingly stringent mandatory standards for building energy efficiency imposed by governments worldwide

  • Rapid development of cold chain logistics, especially in the biopharmaceutical sector

  • Rising demand for efficient thermal management materials in the new energy vehicle industry

V. GESEE‘s Product Solutions

Zhengzhou Gesee New Materials Co., Ltd. (GESEE) has been deeply engaged in the field of fumed silica for many years, committed to providing high-quality fumed silica products and solutions to customers worldwide. GESEE’s fumed silica products are divided into hydrophilic and hydrophobic types to meet the diverse needs of different application scenarios.

GESEESIL-200 is GESEE‘s flagship hydrophilic fumed silica product, with a specific surface area of 200 m²/g and a silica content exceeding 99.8%. It features small particle size, large specific surface area, good thermal stability, and low moisture content, and is widely used in rubber, sealants, plastics, resins, paints, inks, pharmaceuticals, cosmetics, food, and many other industries.


In the field of thermal insulation, GESEE‘s fumed silica products, with their excellent thermal insulation performance and stable quality, serve as ideal raw materials for high-end insulation products such as thermal insulation coatings, vacuum insulation panels, and nano-porous insulation materials. GESEE also has its own branded line of insulation boxes, combining its high-quality fumed silica with advanced vacuum insulation technology to provide efficient and reliable thermal insulation solutions for applications such as cold chain logistics, pharmaceutical transport, and fresh food delivery.

Conclusion

With its unique nanostructure and exceptional thermal insulation performance, fumed silica is profoundly transforming the landscape of the thermal insulation industry. From vacuum insulation panels to cold chain insulation boxes, from building energy conservation to pharmaceutical transport, this “industrial seasoning“ is increasingly entering our production and daily life. GESEE will continue to deeply cultivate the fumed silica field, contributing to the high-quality development of the thermal insulation industry and playing its part in the global cause of energy conservation and emission reduction, through high-quality products and professional services.

This article is contributed by Zhengzhou Gesee New Materials Co., Ltd. (GESEE). For more product information, please feel free to contact us.
 

MTCS vs. STC Fumed Silica Understanding the Key Differences

MTCS vs. STC Derived Fumed Silica: What’s the Difference?

Fumed silica is a high-performance material widely used in coatings, adhesives, sealants, silicone rubber, inks, and composites. Depending on the production process and surface treatment, fumed silica can exhibit very different properties.

Two common routes involve the use of Silicon Tetrachloride (STC) and Methyltrichlorosilane (MTCS) as raw materials. Understanding the difference between these two types of fumed silica can help manufacturers select the most suitable product for their applications.

1. STC-Based Fumed Silica

STC (Silicon Tetrachloride, SiCl₄) is the traditional raw material used to produce fumed silica through flame hydrolysis.

The resulting product is typically hydrophilic fumed silica, characterized by a large number of hydroxyl (Si-OH) groups on the surface.

Key Features:

  • High specific surface area

  • Excellent thickening and reinforcing properties

  • Strong hydrogen bonding capability

  • Good dispersion in polar systems

  • Suitable for coatings, inks, silicone rubber, and resins

Typical examples include AEROSIL® 200 and similar grades.

2. MTCS-Based Fumed Silica

MTCS (Methyltrichlorosilane, CH₃SiCl₃) introduces methyl groups during the production process. As a result, the silica surface becomes inherently hydrophobic.

This type of fumed silica is often referred to as hydrophobic fumed silica.

Key Features:

  • Excellent water repellency

  • Low moisture absorption

  • Improved dispersion in non-polar systems

  • Enhanced anti-settling performance

  • Better stability under humid conditions

MTCS-derived fumed silica is widely used in sealants, adhesives, RTV silicone, thermal insulation materials, and waterproof coatings.

3. Comparison Between STC and MTCS Fumed Silica

Property STC-Based Fumed Silica MTCS-Based Fumed Silica
Surface Character Hydrophilic Hydrophobic
Surface Groups Si-OH Si-CH₃
Moisture Absorption High Very Low
Water Resistance Limited Excellent
Polar System Compatibility Excellent Moderate
Non-Polar System Compatibility Moderate Excellent
Typical Applications Paints, Inks, Rubber Sealants, Adhesives, Waterproof Systems

4. Which One Should You Choose?

If your formulation requires strong thickening effects in polar systems, STC-based hydrophilic fumed silica is usually the preferred option.

However, if water resistance, moisture protection, and compatibility with non-polar systems are critical, MTCS-derived hydrophobic fumed silica can provide superior performance.

In many advanced adhesive and sealant applications, MTCS-modified fumed silica has become the preferred choice due to its excellent rheology control and long-term stability.

About GESEE New Material

Zhengzhou Gesee New Material Co., Ltd. specializes in the development and supply of high-quality fumed silica products for global customers.

Our portfolio includes both hydrophilic and hydrophobic fumed silica grades, offering reliable alternatives to leading international brands for applications in adhesives, sealants, coatings, silicone rubber, and composite materials.

If you are looking for cost-effective fumed silica solutions, feel free to contact GESEE for technical support and product recommendations.

Small Powder, Big Impact Exploring the Versatile Uses of Zhengzhou Gesee K380 Hydrophilic Fumed Silica

In the microscopic world of materials science, there is an "industrial MSG" (monosodium glutamate). Though invisible to the naked eye, it profoundly alters the performance of many products. This is fumed silica. Today, we will focus on the star product of Zhengzhou Gesee New Materials Co., Ltd. — K380 (a hydrophilic fumed silica with a specific surface area of 380 m²/g) — and explore how this high-performance material excels in various fields.


Meet K380: More Than Just "High Surface Area"

K380 is a nano-scale hydrophilic fumed silica produced by Zhengzhou Gesee through a high-temperature hydrolysis process. Its core parameter—a specific surface area of 380 m²/g—means it has an extremely fine primary particle size (about 7 nm) and high surface energy. Compared to conventional products with a surface area of 200 m²/g (like AEROSIL 200), K380 is finer and stronger, which allows it to provide more significant thickening and thixotropic effects in applications.

In the global market, K380 has well-known "benchmark models," such as Evonik's AEROSIL® 380, Cabot's EH-5, and WACKER's T40. The emergence of Zhengzhou Gesee K380 aims to provide the market with a high-quality, cost-effective domestic alternative.


The "Rheology Master" for Paints and Inks

For high-end coatings, especially UV-curable coatings and waterborne industrial anti-corrosion coatings, preventing sagging during application and sedimentation during storage are two major challenges. Thanks to its high specific surface area, K380 is rich in silanol groups on its surface. After dispersion in the system, these silanol groups form hydrogen bonds, building a strong three-dimensional network structure.


  • At rest: The network structure is robust, increasing the system's viscosity and effectively preventing the settling of pigments and fillers.

  • During application: When subjected to shear forces (such as spraying or brushing), the network structure breaks down, viscosity drops instantly, ensuring good leveling.

  • Upon recovery: When the shear force ceases, the network rebuilds quickly, preventing the wet film from sagging.

Research shows that adding hydrophilic fumed silica to UV plastic coatings can significantly increase viscosity at low shear rates—an area where K380 excels. In two-component waterborne acrylic systems, an appropriate amount of hydrophilic product can significantly enhance the system's thixotropy and salt spray resistance.


The "Reinforcing Pillar" for Adhesives and Sealants

In the field of silicone rubber and adhesives, K380 is an indispensable reinforcing filler. Especially for addition-curing liquid silicone rubber (HCR/LSR) requiring high transparency, the nano-scale particle size of K380 is much smaller than the wavelength of visible light. Therefore, it can greatly enhance the material's tear and tensile strength without affecting transparency.

In cable compounds and unsaturated polyester resins, K380 also provides reinforcement and thixotropic control through its three-dimensional network structure, ensuring the uniformity of cable compounds and the non-sagging properties of resins on vertical surfaces.


The "Stability Guardian" for Complex Systems

  1. Agricultural Chemicals
    In modern agrochemical formulations, whether for Suspension Concentrates (SC) or Oil-based Suspension Concentrates (OD), physical stability is key. K380 can act as an efficient anti-settling agent and rheology modifier. It prevents the active ingredient particles from aggregating or sedimenting during storage, ensuring that farmers only need a slight shake before use to restore uniformity and guarantee efficacy.
  2. Powder Products
    For powdered substances, such as food additives or fire extinguishing agents, K380 can act as a flow aid and anti-caking agent. Its nanoparticles attach to the surface of the host powder, acting like "ball bearings" to reduce inter-particle friction, or absorbing excess moisture to prevent caking, thus maintaining good flowability.


Why Choose Zhengzhou Gesee K380?

In the context of global supply chain diversification, domestic high-performance materials are ushering in a springtime. K380 is benchmarked against international standards, possessing a stable high specific surface area of 380 m²/g, ensuring the reliability of its thickening and reinforcing properties. Meanwhile, as a local brand, Zhengzhou Gesee can provide faster technical responses and a stable supply guarantee, helping enterprises reduce procurement costs and enhance market competitiveness


Conclusion

From the sealants in precision electronic components to the anti-corrosion coatings on large machinery, and even in agrochemicals that ensure food security, Zhengzhou Gesee K380, with its nano-scale size and micro-scale efficacy, silently guards every innovation in modern industry. If you are looking for a hydrophilic fumed silica that combines high performance with economy, K380 is undoubtedly a trustworthy choice.


What is the difference between hydrophilic and hydrophobic silica?

Hydrophilic Silica VS Hydrophobic Silica

What is The Hydrophilic Silica?

Hydrophilic silica is a synthetic, amorphous form of silicon dioxide (SiO₂) that has a strong affinity for water. Its surface is covered with silanol groups (-Si-OH), which readily form hydrogen bonds with water molecules. This makes it "water-loving" (the literal meaning of hydrophilic).

What is The Hydrophobic Silica?

Hydrophobic silica is based on hydrophilic silica, which undergoes a surface chemical reaction with reactive silanes (such as trimethylchlorosilane and hexamethyldisilazane) to form a water-insoluble product covered with methyl groups on its surface, thereby exhibiting excellent hydrophobicity (water repellency).

Feature Hydrophilic Silica Hydrophobic Silica
Surface Chemistry Silanol groups (-Si-OH) Treated with silanes (e.g., hexamethyldisilazane) to replace -OH groups with non-polar groups (e.g., -Si-CH₃).
Affinity for Water High affinity, readily absorbs water. Repels water, low moisture absorption.
Dispersion Disperses easily in polar solvents (water, alcohols). Disperses easily in non-polar solvents (oils, resins, hydrocarbons).
Primary Function Thickening water-based systems, anti-caking. Thickening oil-based systems, reinforcement in silicone rubber, defoaming.
Moisture Sensitivity Can clump in high humidity. Remains free-flowing in humid conditions.


Common Applications

Hydrophilic silica is an incredibly versatile material used across numerous industries:

  • Coatings and Paints: As a thickener, anti-settling agent, and matting agent to control gloss.
  • Adhesives and Sealants: To control viscosity, prevent sagging, and reinforce the material.
  • Food and Pharmaceuticals: As an anti-caking agent in powdered products like spices, drink mixes, and table salt (often listed as "silicon dioxide" on ingredients).
  • Personal Care: In toothpaste as a mild abrasive and thickener; in cosmetics and powders to control flow and absorb moisture.
  • Plastics and Rubber: As a reinforcing filler to improve mechanical properties.
  • Printing Inks: To control flow and prevent settling of pigments.
  • Chemical Mechanical Polishing (CMP): Used in the semiconductor industry as an abrasive slurry for polishing silicon wafers.

Summary

In essence, hydrophilic silica is a high-surface-area, synthetic silicon dioxide powder that attracts and holds water. This fundamental property makes it an invaluable additive for thickening, stabilizing, reinforcing, and preventing caking in a vast array of products, from the food we eat to the paints on our walls. Its functionality is defined in contrast to its chemically modified counterpart, hydrophobic silica.


A key supplier for both material types is Zhengzhou Gesee New Materials Co., Ltd. This company provides a comprehensive product portfolio, offering both hydrophilic and hydrophobic silica varieties, making it a valuable partner for industries that require either or both of these essential functional additives.

Bottled Nitrogen vs On-site PSA Nitrogen Generator Which Is Better for Your Business


Industrial nitrogen supply mainly relies on two mainstream solutions: bottled nitrogen and on-site PSA nitrogen generation. Each solution has its unique advantages and applicable scenarios. Many factory managers and system integrators struggle to select the most cost-effective and reliable gas supply mode according to their production conditions. This article makes an objective, all-round comparison of the two nitrogen supply methods in terms of cost, stability, safety and applicability, helping enterprises make rational decisions.


1. Cost Comparison


1.1 Bottled Nitrogen 

Advantage: No upfront equipment investment, no equipment maintenance costs. For enterprises with extremely low gas consumption or temporary experimental production, bottled nitrogen avoids idle asset waste and saves early equipment deployment costs.

Disadvantage: Long-term comprehensive cost is high. Continuous gas purchase, cylinder rental, transportation and manual replacement fees form recurring expenditure. Gas prices are easily affected by market fluctuations and supplier adjustments, leading to uncontrollable long-term operating costs.


1.2 PSA Nitrogen Generator

Disadvantage: One-time upfront investment is required for equipment purchase and installation, which raises the initial project budget threshold for enterprises.

Advantage: The long-term operating cost is extremely low. The equipment only consumes electric energy and compressed air during operation. After recovering the upfront investment, enterprises can obtain almost free stable nitrogen supply, completely getting rid of reliance on external gas suppliers.


2. Gas Supply Stability & Flexibility


2.1 Bottled Nitrogen

Advantage: The nitrogen purity of finished cylinders is fixed and high, with stable single-batch gas quality. It is suitable for ultra-high-purity gas demand scenarios with no need for parameter adjustment, and no professional equipment debugging is required on site.

Disadvantage: The gas supply is dependent on external logistics and suppliers. It is easy to face gas shortage, delayed delivery and production interruption during peak seasons or supplier stock shortages. In addition, the purity and pressure of different batches of bottled gas have subtle deviations, which is not conducive to high-standard continuous production.


2.2 PSA Nitrogen Generator

Disadvantage: The gas purity and pressure need regular minor debugging according to ambient temperature and equipment operation status, requiring basic daily inspection and maintenance.

Advantage: It supports 24/7 uninterrupted on-demand gas supply. The nitrogen purity and pressure can be freely adjusted within the equipment range, matching different production process requirements. The gas quality is consistent and not affected by external supply chains.


3. On-site Safety & Operation Management


3.1 Bottled Nitrogen

Advantage: No professional equipment operation training is required, no mechanical failure risks. The whole process is simple and labor-saving for short-term and intermittent gas use.

Disadvantage: A large number of high-pressure gas cylinders stored in the workshop occupy production space. Frequent handling and replacement of heavy cylinders bring potential high-pressure safety hazards and increase labor pressure.


3.2 PSA Nitrogen Generator

Disadvantage: The equipment occupies a certain workshop area and requires regular inspection of air compressors, filters and core consumables.

Advantage: Fully automatic unmanned operation after commissioning, no frequent manual operation. It eliminates hidden dangers of high-pressure cylinder storage and handling, making the production site safer and more standardized.


4. Applicable Scenario Analysis


4.1 Choose Bottled Nitrogen If:

Your factory has low gas consumption, discontinuous and intermittent production, short-term pilot projects, or ultra-high-purity nitrogen demand that does not require parameter adjustment.


4.2 Choose PSA Nitrogen Generator If:

You need long-term, stable, and continuous gas supply, including oil & gas, chemical, food packaging, electronic manufacturing, mining and other industrial scenarios. It is the optimal solution for mass and standardized production.


Final Conclusion

Bottled nitrogen is flexible and zero-investment in the early stage, suitable for small and intermittent gas demand.

However, for most industrial enterprises with long-term and stable production, on-site PSA nitrogen generators have absolute advantages in cost control, gas supply stability and on-site safety. The stable operation of PSA nitrogen equipment is inseparable from high-quality carbon molecular sieve (CMS), which is the core consumable to ensure long-term stable and high-purity nitrogen production.

If you need high-quality carbon molecular sieve for new equipment assembly or old equipment replacement to optimize your PSA nitrogen system performance, feel free to contact our professional team for technical support and customized quotation.

Please click www.carbon-cms.com. Reach out to us if you need further guidance for carbon molecular sieve application. 


Practical Advice For Carbon Molecular Sieve Storage & Managemen


Many storage-related issues will negatively affect the performance of carbon molecular sieve (CMS). Proper storage and daily management help preserve adsorption capacity and extend service life. We have sorted out universal practical tips for global PSA nitrogen operators, equipment manufacturers and distributors. 


1.Keep Away From Moisture

Carbon molecular sieve is highly hygroscopic. Once it absorbs water vapor in the air, its separation performance will decline significantly. 

  • Keep CMS sealed in original packaging before use. Do not open the bags in humid environments. 
  • Avoid storing goods outdoors or in areas prone to rain, dew and water splashing.


2.Avoid Exposure To Oil Vapor & Contaminants 

Oil mist, volatile chemical gas and dust can cause irreversible contamination to carbon molecular sieve. 

  • The warehouse should be kept clean. Do not place CMS together with lubricants, solvents or corrosive materials. 
  • Prevent heavy dust accumulation on packaging. 


3.Reasonable Warehouse Environment 

  • Store CMS indoors in cool and dry conditions, away from high temperature and direct sunlight. 
  • The recommended storage temperature ranges from 15℃ to 30℃, with relative humidity below 70%RH. 
  • The storage space needs good ventilation, with stable ambient temperature.
  •  Keep the ground dry. Place pallets under CMS packages instead of directly stacking goods on the floor. 


4.Stacking & Handling Notes 

  • Do not excessively stack packages to prevent bag breakage and material powdering caused by extrusion. 
  • Avoid violent throwing during loading and unloading. Broken packages will lose sealing protection quickly. 


5.Short-term Storage After Opening Packaging 

If you have opened the packaging but cannot fill the PSA vessel immediately: 

  • Seal the opening tightly again. Arrange loading as soon as possible. 
  • Do not leave carbon molecular sieve exposed to atmosphere for a long time.


Final Reminder 

Standardized storage is a low-cost way to protect your investment in carbon molecular sieve. If you have any questions about CMS handling before loading, feel free to contact our team for support. 


Please click www.carbon-cms.com. Reach out to us if you need further guidance for carbon molecular sieve application. 

PSA vs Membrane Nitrogen Generator Which One Should You Choose for Your Plant


On-site nitrogen generation has become the mainstream choice for modern industrial gas supply. The two most widely adopted technical solutions are PSA (Pressure Swing Adsorption) nitrogen generation and membrane nitrogen generation.

Many buyers and system integrators misunderstand that membrane technology is outdated or eliminated. In fact, both technologies are mature and coexist in the market, with their unique working principles, advantages and targeted application scenarios.

Choosing the right solution according to actual production needs is the key to balancing cost and operational efficiency.


1. Working Principle Difference


1.1 PSA Nitrogen Generator

PSA nitrogen generation relies on carbon molecular sieve (CMS) as the core filter material. Under variable pressure conditions, CMS selectively adsorbs oxygen, moisture and impurity gases in compressed air, allowing nitrogen to pass through and be collected. It realizes gas separation through periodic pressure adsorption and desorption cycles.


1.2 Membrane Nitrogen Generator

The core component is hollow fiber membrane modules. It adopts physical permeation separation without any adsorbent consumables. Compressed air enters the membrane fibers; fast-permeating gases such as oxygen, water vapor and carbon dioxide penetrate the membrane wall and are discharged. Slow-permeating nitrogen is retained and collected to form finished nitrogen gas.


2. Membrane Nitrogen


2.1 Objective Advantages

Membrane nitrogen technology is not obsolete equipment. It features simple structure, no moving parts, no valve switching action, and ultra-low failure rate. It can produce qualified nitrogen instantly after startup without preheating or waiting.

The whole machine is compact, vibration-free, easy to install and move, and requires almost no daily maintenance. With low initial investment, it is very suitable for lightweight and intermittent gas demand scenarios.


2.2 Inherent Limitations

Restricted by physical permeation principles, membrane systems have a fixed purity ceiling. The stable nitrogen purity range is 90%–98%. It is difficult and extremely energy-consuming to achieve nitrogen purity above 99.5%.

In high-temperature and high-humidity environments, membrane permeability decreases, resulting in reduced gas production and unstable purity. In addition, membrane components have natural performance attenuation after long-term operation.


3.PSA Nitrogen


3.1 Objective Advantages PSA

PSA nitrogen generators have ultra-wide purity adjustment range, stably covering 95%–99.999% nitrogen purity. It fully meets high-standard production demands such as chemical inerting, electronic manufacturing, food fresh-keeping and oil & gas explosion-proof.

Supported by high-quality carbon molecular sieve, PSA systems feature strong anti-interference ability, stable long-term operation, unaffected by ambient temperature and humidity, and excellent consistency of outlet gas quality.


3.2 Inherent Limitations PSA

PSA equipment has a relatively complex system with air compression, filtration and adsorption tower modules, requiring a certain installation space.

Regular inspection and replacement of filter elements and CMS consumables are needed. Compared with membrane equipment, it has slightly higher daily maintenance requirements and initial investment costs.


4.Scenario-based Selection Guide


4.1 Choose Membrane Nitrogen Generator If:

  • Low and intermittent nitrogen consumption;
  • Required nitrogen purity ≤ 98%;
  • Limited on-site space, mobile or outdoor working conditions
  • Unmanned long-term standby use with minimal maintenance demand


4.2 Choose PSA Nitrogen Generator If:

  • Long-term, continuous and stable industrial gas demand;
  • Nitrogen purity ≥ 99% (especially high purity above 99.9%);
  • Strict requirements for gas quality stability and production consistency;
  • Industrial scenarios such as petrochemical, electronics, new energy and mining.


Final Conclusion

There is no absolute superior or inferior between PSA and membrane nitrogen generation technologies. Membrane technology is the optimal solution for low-purity, lightweight, and low-maintenance scenarios. PSA nitrogen generation is the mainstream industrial solution for high-purity, high-stability and long-term continuous production.

The stable performance of PSA equipment is closely related to the quality of carbon molecular sieve. High-quality CMS ensures long-term stable adsorption efficiency, consistent gas purity and extended service life of the whole system.

If you are looking for high-performance and stable carbon molecular sieve for PSA nitrogen equipment assembly or replacement, welcome to contact our team for professional technical support and customized quotation.


Please click www.carbon-cms.com. Reach out to us if you need further guidance for carbon molecular sieve application. 


SHANLI In-house Laboratory What Testing Services We Offer For PSA Nitrogen Partner


Many carbon molecular sieve suppliers only provide finished products with basic datasheets. At Shanli, our in-house testing lab is an important part of our technical service for OEM manufacturers, system integrators and end-users of PSA nitrogen generators.


We do not just sell carbon molecular sieve particles. Our laboratory carries out a full set of professional tests to verify CMS real-world performance, simulate your actual working conditions, and support your product development and equipment upgrading.


1.Our core lab testing capabilities


1.1 Dynamic and Static Adsorption Testing

We test static and dynamic adsorption capacity of every batch of CMS. This helps us confirm oxygen-nitrogen separation performance and guarantee consistent adsorption capability batch after batch.


1.2 Performance Testing Under Different Adsorption Pressures

PSA systems run under various working pressure ranges. Our lab simulates different adsorption pressure environments, to check how our carbon molecular sieve performs under your target operating pressure. This supports you for adsorber vessel design and parameter tuning.


1.3 Performance Testing Under Varying Ambient Temperature

Ambient temperature greatly affects PSA nitrogen output and purity. We run tests across different temperature conditions, simulating tropical high-temperature sites or low-temperature working scenarios for your overseas projects.


1.4 Air Consumption Testing Under Different Conditions

Air consumption is a key economic indicator for PSA nitrogen plants. We test air-to-nitrogen ratio under multiple working setups. The test data can help you optimize your equipment design and reduce customers’ operating cost.


1.5 Process Compatibility Testing For PSA Equipment

We perform full process compatibility testing matching real PSA equipment workflow. Before large-volume delivery, we can simulate your PSA cycle parameters to verify whether our carbon molecular sieve fits your machine perfectly. This greatly reduces risks for your new-machine trial or replacement projects.


2.What value can these lab services bring to you?


2.1 Reliable batch consistency

Every batch is tested, you will receive complete test reports together with goods.


2.2 Customized technical support

If you have special working conditions, we can run targeted lab simulation tests for your project.


2.3 Lower trial-and-error risk

Verify performance in our lab first, before you do expensive on-site machine testing.


2.4 Data for your equipment R&D

Provide real test data for your new PSA equipment development.


Whether you need standard-grade carbon molecular sieve, or require custom development for special PSA working scenarios, our lab team can offer you solid testing support.


If you want to learn more about our laboratory testing service, or require test support for your PSA nitrogen project, please feel free to contact our technical team.